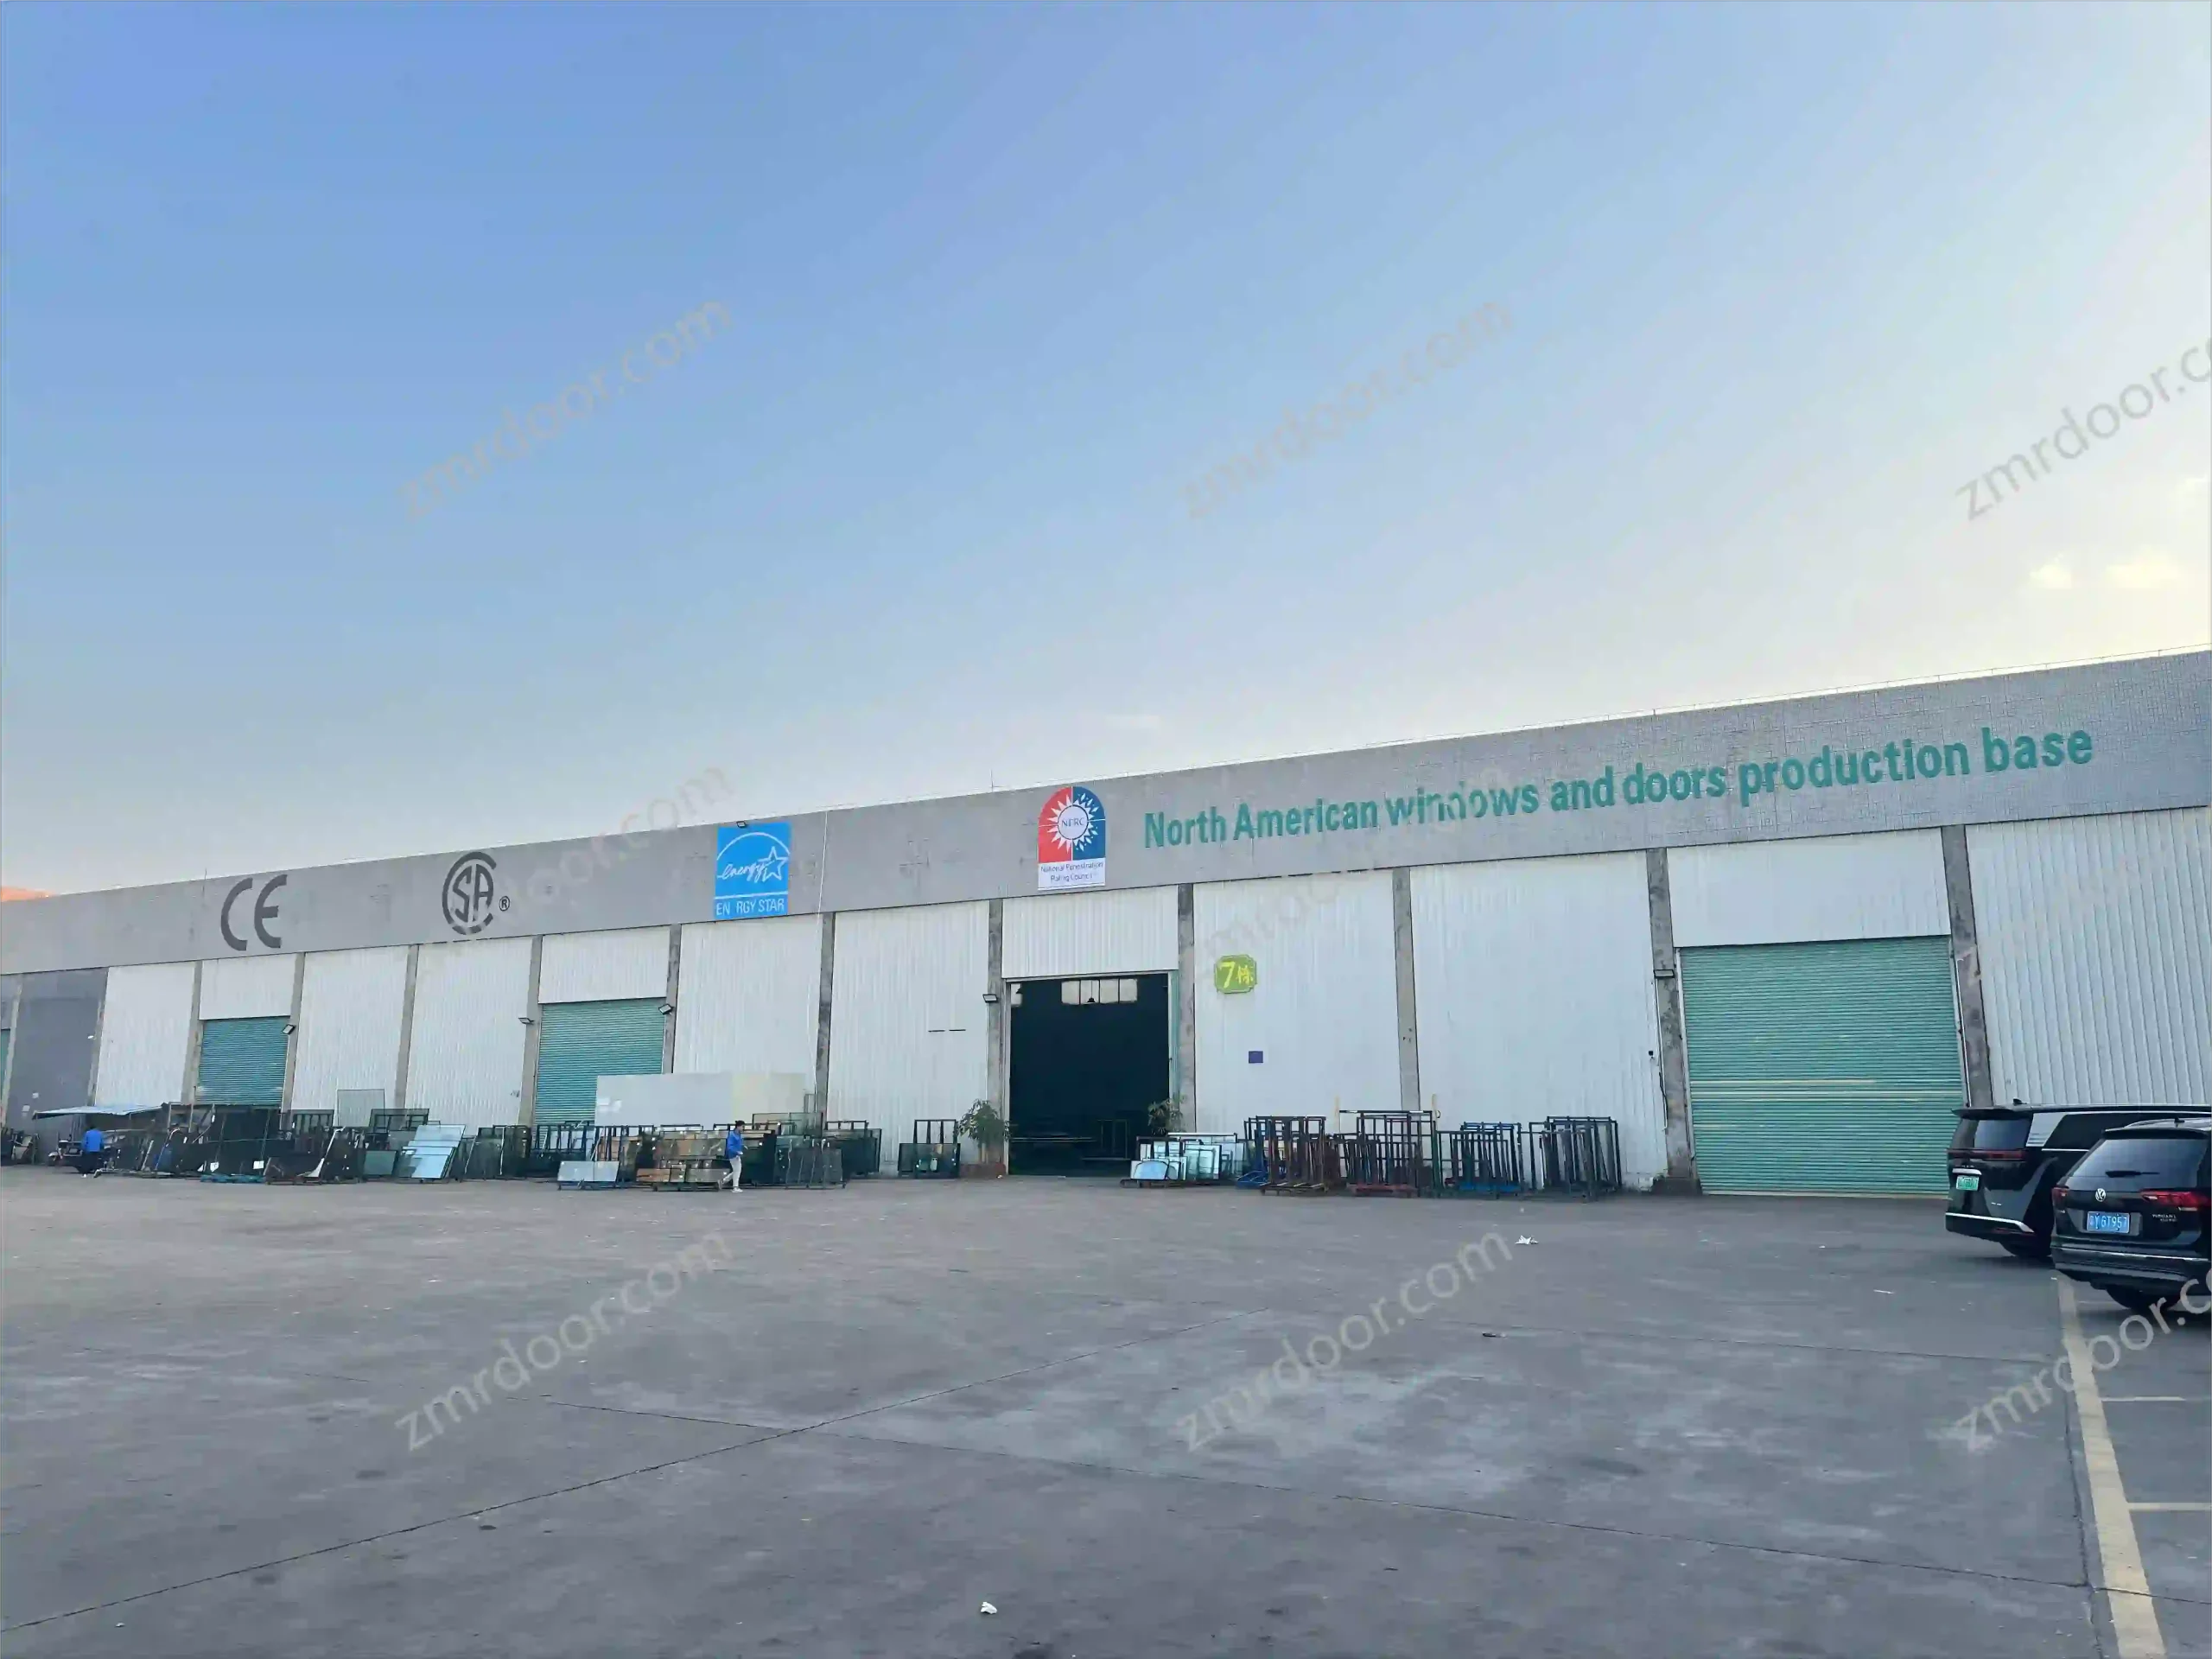
Featured OEM Architectural Aluminium Systems
Explore factory-direct thermal break windows, acoustic partitions, double-glazed sliding doors, and custom fenestration engineered for global infrastructure standards.
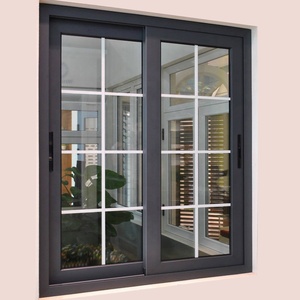
New Design Double Glazed Aluminium Profile Sliding Windows With Grid
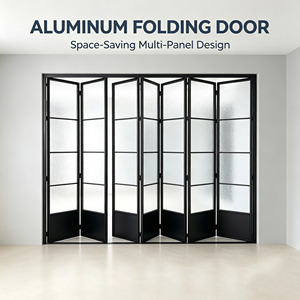
Aluminum Alloy Waterproof Folding Sliding Door Minimalist Partition for Kitchen Living Room Balcony with 5 Year Warranty
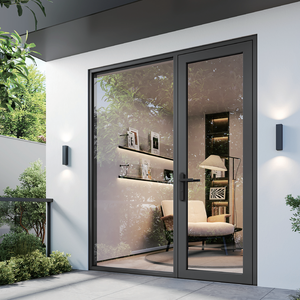
Australian Standard AS2047 Certificated Luxury Swing Door Thermal Break Double Glazed Tempered Glass Casement Aluminum Doors
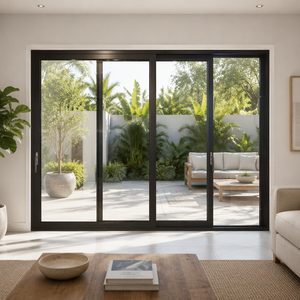
Aluminium Sliding Door with Double Glazing Tempered Glass Modern Design Sound Insulation Workshop Use Apro Brand
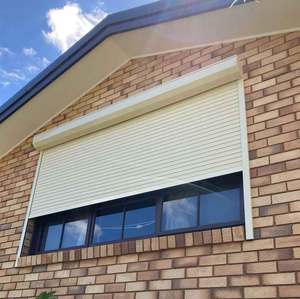
Customized Front Window Security Roller Shutter Shop Aluminum Alloy Remote Control Aluminum Windows with Roller Shutter Window
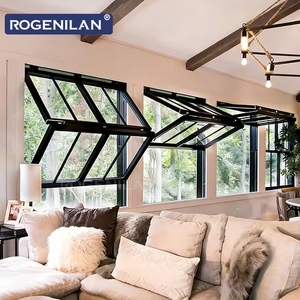
Fold Up Black Aluminum Tempered Double Glass Accordion Horizontal Folding Window Glazed Vertical Bifold Windows
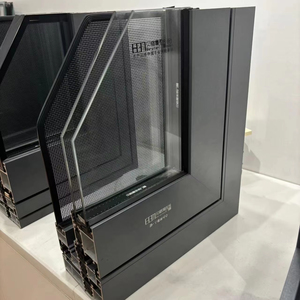
Beigeman Modern Double Glazed Aluminium Casement Windows High Quality Soundproof Tempered Glass for House Villas Kitchen Hotel
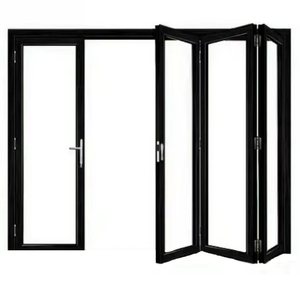
Folding Style Cheap Aluminum Interior Acrylic Folding Door Customize Size Color Accordion Kitchen Livingroom Folding Glass Doors
Custom OEM Aluminium Partition With Door Factories: Engineering Whitepaper
A comprehensive analysis of structural extrusion alloys, thermal break insulation mechanics, acoustic isolation, and global B2B procurement benchmarks for enterprise project buyers.
1. The Evolution of Architectural OEM Aluminium Partitions & Integrated Door Systems
Modern commercial and luxury residential developments demand a rigorous balance between visual minimalism, acoustic privacy, structural load resistance, and thermal efficiency. As international building codes tighten around energy consumption (U-factor thresholds) and physical durability (wind-load and water tightness), sourcing from specialized Custom OEM Aluminium Partition With Door Factories & Factory networks has transitioned from simple commodity purchasing to deep engineering collaboration.
Factory-direct OEM/ODM production, particularly centered in manufacturing hubs like Foshan, Guangdong, provides global importers, commercial contractors, and project developers with tailored fenestration systems. Unlike off-the-shelf prefabricated units, custom engineered architectural aluminium partition systems incorporate precise extrusion profiles, specialized glass build-ups, and heavy-duty concealed hardware to satisfy exacting project schedules.
2. Material Science & Structural Metallurgy of Extrusion Profiles
At the core of high-performance architectural partitions and door systems lies the chemical composition and heat treatment of the aluminium alloy profile. Leading OEM factories utilize 6063-T5 or 6063-T6 primary aluminium billets, engineered for optimal tensile strength, corrosion resistance, and surface finishing quality.
| Profile Metric | Standard Commercial Grade | Veltor OEM Project Specification | Engineering Advantage |
|---|---|---|---|
| Alloy & Temper | 6063-T5 Standard Recycled Billet | 6063-T6 Primary Pure Aluminium | Higher yield strength (>170 MPa) & structural rigidity for high-span walls. |
| Profile Wall Thickness | 1.2mm – 1.4mm | 2.0mm – 3.0mm Heavy-Duty Series | Prevents deflection under high wind loads & supports heavy double-glazed sashes. |
| Thermal Break Strip | PVC / Low-Grade Resin Injection | Polyamide PA66 GF25 (25% Glass Fiber) | Matches coefficient of thermal expansion of aluminium; resists structural shear. |
| Acoustic Rating (STC) | STC 28 – 32 dB | STC 42 – 48 dB (with acoustic PVB) | Eliminates office cross-talk & urban noise pollution in high-rise applications. |
| Surface Finishing | Basic Anodizing / Standard Powder Coating | PVDF Fluorocarbon (AAMA 2605) / Anodized 25μm | 30+ year resistance to UV degradation, salt spray, and industrial pollutants. |
3. Acoustic & Thermal Performance Mechanics in Interior Partitions & Exterior Doors
In enterprise office partitions and residential multi-slide interior transitions, acoustic isolation is paramount. High-grade OEM aluminium partition factories achieve superior Sound Transmission Class (STC) ratings through multi-cavity extrusion geometry, double EPDM (Ethylene Propylene Diene Monomer) gasket compression seals, and specialized insulated glass units (IGU).
By pairing laminated glass configurations featuring acoustic Polyvinyl Butyral (PVB) or Sound-Dampening Interlayers with thermal-break aluminium framing, factory engineers eliminate acoustic flanking paths while drastically reducing solar heat gain coefficients (SHGC). In cold climates, double or triple glazing filled with 90%+ Argon gas lowers overall U-values down to 1.2 W/m²K, directly contributing to LEED and BREEAM building certifications.
Future Global Procurement Trends in Aluminium Partitions & Doors
Key macro shifts shaping how commercial developers, architects, and importers source OEM/ODM fenestration systems over the next decade.
1. Decarbonization & Low-Carbon Aluminium Sourcing
Global B2B buyers are requiring Environmental Product Declarations (EPDs) and low-carbon aluminium extruded via renewable energy (hydroelectric smelting). OEM factories capable of tracking carbon intensity per metric ton gain distinct competitive advantages in international tenders.
2. Ultra-Slim Sightlines & Invisible Frame Architectures
Minimalist interior partitions featuring narrow face widths (as thin as 15mm–20mm interlocks) are becoming the global design default. Factories must engineer heavy-duty concealed stainless steel rollers and concealed floor tracks to carry glass sashes exceeding 400kg.
3. Smart Glass & Building Automation Integration
The convergence of Polymer Dispersed Liquid Crystal (PDLC) switchable smart glass, motorized sliding mechanisms, and biometric access control directly within custom OEM aluminium door profiles is accelerating across executive boardrooms and luxury residences.
4. Digital Twin BIM & Pre-Engineering Verification
Modern procurement mandates 3D BIM (Building Information Modeling) objects and computer-simulated structural stress testing before extrusion dies are cut. Direct-to-factory shop drawing approvals drastically reduce field installation errors.
5. Modular Off-Site Construction & Knock-Down (KD) Packaging
To minimize overseas shipping volume and avoid glass breakage in transit, enterprise buyers favor factory pre-assembled frame components designed for rapid, error-free site assembly with color-coded hardware kits and labeled opening numbers.
Factory Superiority: Why Overseas Importers Partner With Veltor
Operating from Nanhai District, Foshan—China's industrial heartland for architectural aluminium extrusion—Veltor Window & Door Co., Ltd. delivers direct factory capabilities without middleman markups.
Choosing the right OEM partner requires validating raw material supply chains, processing machinery precision, quality control systems, and export compliance certifications. Below is a breakdown of our industrial capabilities engineered to safeguard global project execution:
Foshan Extrusion Ecosystem
Located in Shishan Town, Nanhai, our facility benefits from immediate access to top-tier billet casters, anodizing lines, and hardware manufacturers, slashing lead times for custom extrusion dies to under 14 days.
CNC Machining Precision
Double-head precision cutting saws and 5-axis CNC machining centers guarantee profile cutting tolerances within ±0.5mm, ensuring seamless 45-degree corner crimping and perfect lock mortise alignment.
Certified Quality Standards
Our manufacturing processes align with ISO 9001 quality management, Australian AS2047, European CE EN 14351-1, and North American NFRC energy performance testing criteria.
Comprehensive Pre-Shipment QC
Every partition frame and door sash undergoes pre-assembly on factory test rigs, verifying water tightness, smooth roller sliding action, sash alignment, and hardware torque before packaging.
Reinforced Export Packaging
Frames are protected with PE protective film, heavy-duty corner guards, non-scratch EPE foam layer, and packed into fully enclosed fumigated wooden crates labeled with precise installation mark numbers.
Dedicated Engineering Support
Our in-house technical department translates architectural CAD schedules into detailed shop drawings, glass stress calculations, and installation guides for seamless field execution.
Frequently Asked Questions (FAQ) for OEM Procurement
Technical and logistical insights to help project directors, contractors, and distributors streamline factory direct ordering.
What is the Minimum Order Quantity (MOQ) for custom OEM aluminium partition and door orders?
Because Veltor engineers every fenestration system to custom architectural dimensions, we do not restrict buyers to rigid retail MOQs. For custom project orders, the pragmatic baseline is governed by container shipping economics (LCL vs. FCL consolidation). We accommodate single-project villa orders as well as full multi-container dealer shipments, providing customized freight engineering to maximize container volume utilization.
How do you ensure thermal-break partitions perform in extreme temperature zones?
Our thermal break aluminum systems incorporate high-grade Polyamide PA66 GF25 insulating strips mechanically crimped between the interior and exterior aluminum extrusions. Combined with double or triple insulated glass units (IGU) featuring Low-E coatings, warm-edge composite spacers, and argon gas infill, our systems prevent thermal bridging, stop condensation formation, and lower heating/cooling HVAC energy demands in both desert heat and arctic cold climates.
Can your factory manufacture windows and doors compliant with local wind load and building standards?
Yes. Prior to production, our engineering team evaluates your project's specific geographic parameters, including structural wind pressure (Pascal ratings), water penetration resistance, air infiltration limits, and safety glazing mandates (such as Australian AS2047, European CE, or North American NAFS standards). We issue comprehensive CAD shop drawings detailing profile cross-sections, wall thicknesses, and glass specs for engineer-of-record approval.
What custom surface finishes and color-matching services are available for OEM extrusions?
We provide a comprehensive array of architectural surface treatments, including Qualicoat-certified electrostatic powder coating (RAL color spectrum), PVDF fluorocarbon coatings for harsh coastal marine environments, mechanical anodizing (15μm to 25μm film thickness), fine-grain sandblasting, and realistic thermal-transfer wood-grain textures. Custom color matching against architectural physical swatches is available upon request.
What is the typical lead time for prototype die creation and mass production?
For standard profile series, production lead time is typically 25 to 35 calendar days following CAD shop drawing sign-off and deposit receipt. For specialized custom OEM profiles requiring new extrusion die tooling, die creation and sample extrusion testing take approximately 12 to 15 days, followed by standard mass production schedules.
How are fragile glass partitions and door assemblies packaged for trans-oceanic transport?
Export packaging is engineered to eliminate transit damage. Extrusion frames are wrapped in anti-scratch protective film and fitted with heavy-duty plastic corner guards. Glass units are packed separately or pre-glazed using rubber setting blocks and structural silicone, then secured inside fully enclosed, ISPM-15 compliant fumigated plywood crates equipped with forklift entry channels and moisture-absorbing desiccant packs.
Ready to Source Precision OEM Aluminium Partitions & Doors?
Submit your window schedule, architectural drawings, or RFQ specifications directly to our engineering factory team for a comprehensive technical quote and shop drawing review within 24 hours.